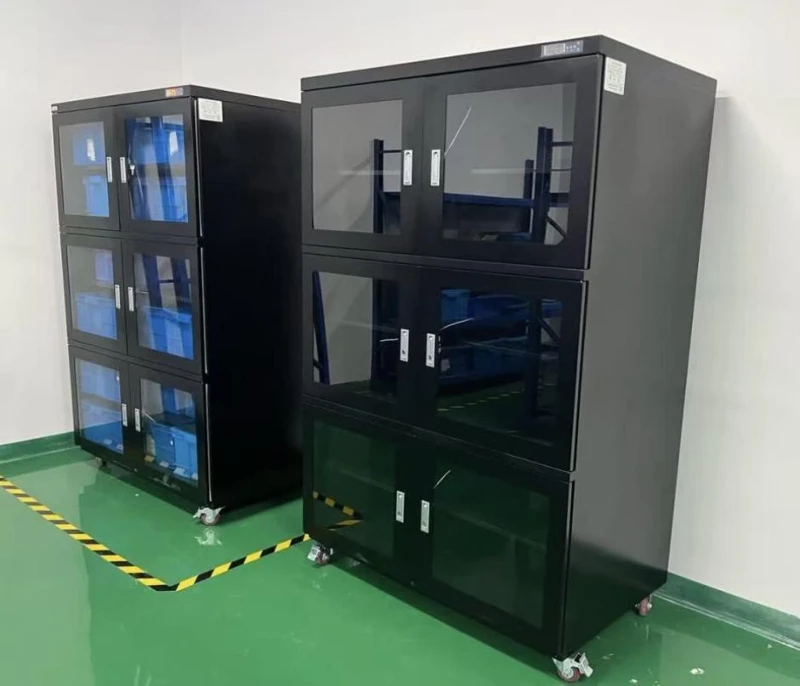
The Smart Moisture Proof Cabinet (commonly referred to as an electronic dry cabinet or humidity-controlled cabinet) is a professional storage solution designed to automatically and precisely control internal humidity, protecting moisture-sensitive items.
Unlike traditional passive moisture protection using desiccants, this cabinet is built around intelligent humidity control and active dehumidification, ensuring long-term, reliable protection.
Product Advantages
1. Precise and Stable Control – Risk Prevention at the Source
Like a precision "humidity-controlled chamber," the cabinet maintains humidity at a preset target level (for example, 40–50% RH for camera lens storage) with accuracy up to ±1%–3% RH. This level of stability is critical for protecting sensitive items by preventing lens fungus, chip oxidation, and paper embrittlement.
2. Active Dehumidification – Set Once, Worry-Free
Using semiconductor condensation or physical adsorption technology, the cabinet continuously removes moisture from the interior. Simply plug in the unit and set the desired humidity level to achieve true long-term operation-eliminating the risk of forgetting to replace desiccants and the resulting damage.
3. Intelligent Management – Efficient and Convenient
This is where the "smart" aspect truly stands out. Features include digital displays, alarm alerts for humidity deviations, and data logging. High-end models support mobile app remote monitoring, allowing users to track storage conditions anytime and anywhere, significantly improving management efficiency and peace of mind.
4. Comprehensive Safety and Protection
- Physical Protection: Constructed from cold-rolled steel, tempered glass, and reliable locking mechanisms to provide strong anti-theft and impact resistance.
- Anti-Static Protection: Internal shelves are often treated with anti-static coatings, which is essential for storing precision electronic components such as chips and circuit boards.
- Power-Off Protection: Cabinets using physical adsorption technology can maintain a low-humidity environment for dozens of hours after a power outage, offering additional safety assurance.
5. Economical and Durable – Long-Term Value
Although the initial investment may be higher, no consumables are required. A high-quality moisture-proof cabinet can be used for over ten years, resulting in a much lower long-term annual cost compared to traditional methods. More importantly, it provides invaluable protection for high-value items by preventing irreversible moisture-related losses.

Specifications
|
Item |
Specification |
|
|
Model |
Smart Moisture Proof Cabinet |
|
|
Material |
Stainless Steel, Cold-Rolled Steel Sheet |
|
|
Surface Treatment |
Coating (Powder / Paint), Film Lamination |
|
|
Applicable Environments |
Construction Sites, Public Facilities, Industrial Plants, Laboratories, Medical and Office Environments |
|
|
Key Features |
Durability, Corrosion Resistance, Safety |
Application Scenarios
I. Electronics Manufacturing and Precision Storage
Electronic Components and Precision Devices: Integrated circuits, sensors, and similar components are highly sensitive to moisture. The cabinet effectively prevents oxidation and short circuits.
Laboratory Sample Storage: Microscopes, analytical instruments, and other laboratory equipment require stable humidity conditions.
II. Photography and Valuable Item Storage
Photography Equipment: Cameras and lenses are prone to moisture damage during long-term storage. The cabinet significantly extends equipment lifespan.
Watches and Jewelry: Metal products are susceptible to corrosion; the cabinet provides an ideal storage environment.
III. Scientific Research and Industrial Environments
- Laboratory Equipment: Ensures measurement accuracy by maintaining stable humidity.
- Power Equipment Protection: Prevents condensation in switch cabinets, reducing the risk of short circuits.
- Data Centers: Controls cabinet humidity to protect servers and electronic systems.
- Chemical Industry Equipment: Protects instruments and control valves in corrosive gas environments.
IV. Medical and Specialized Fields
Precision Medical Devices: Equipment such as endoscopes requires reliable moisture protection.

Material Characteristics
1. Cold-Rolled Steel Sheet
Offers high strength, good formability, and cost efficiency. It forms the main structural frame and provides basic protection. After rust-resistant surface treatment (such as epoxy coating), it delivers reliable corrosion resistance.
2. Stainless Steel (e.g., 304 Grade)
Provides excellent corrosion resistance, high strength, easy cleaning, and a premium appearance. It is ideal for industrial, laboratory, or coastal humid environments. While more expensive, it offers an exceptionally long service life.
FAQ
Q: What are the main materials used in this Stainless Steel Smart Nitrogen Gas Cabinet?
A: A smart moisture-proof cabinet is not merely a container but a precisely engineered system designed to maintain a stable, low-humidity microenvironment. Its design focuses on four core objectives: structural durability, airtight sealing, operational safety, and professional-level protection.
Hot Tags: smart moisture proof cabinet, China smart moisture proof cabinet manufacturers, suppliers, Smart Moisture Proof Cabinet, smart nitrogen gas cabinet, Stainless Steel Smart Nitrogen Gas Cabinet